How to Lower Paint Brush Production Costs Without Hurting Quality
Sep 07, 2026
For many paint brush manufacturers, cutting costs almost always means cutting corners on materials. It seems like the easiest way to squeeze margins is to use cheaper bristles, thinner ferrules, or lower-grade components. But this approach almost always backfires: it leads to higher rejection rates, more customer returns, and a damaged brand reputation. The truth is, most waste in brush production happens in hidden, process-related areas—not in the visible raw materials. With targeted adjustments to material selection, dimensional control, and assembly efficiency, you can reduce total costs without sacrificing product quality.
Wedge material is one of the most underrated cost drivers in brush production. Traditional wooden wedges have low upfront material cost, but they carry heavy hidden expenses. They absorb moisture and swell, causing uneven bristle tension and “fish mouth” defects that raise scrap rates. They also splinter during machine insertion, jamming equipment and creating unplanned downtime. Virgin plastic wedges solve these issues but come at a premium price.
PE regrind wedges strike the optimal balance. Made from recycled polyethylene processed to tight specifications, they deliver the same dimensional stability, moisture resistance, and machine compatibility as virgin PE, but at a significantly lower material cost. They run cleanly on automated assembly lines, produce no splinters, and maintain consistent bristle packing batch after batch. For an internal component hidden inside the ferrule, there is no quality tradeoff—only cost savings.
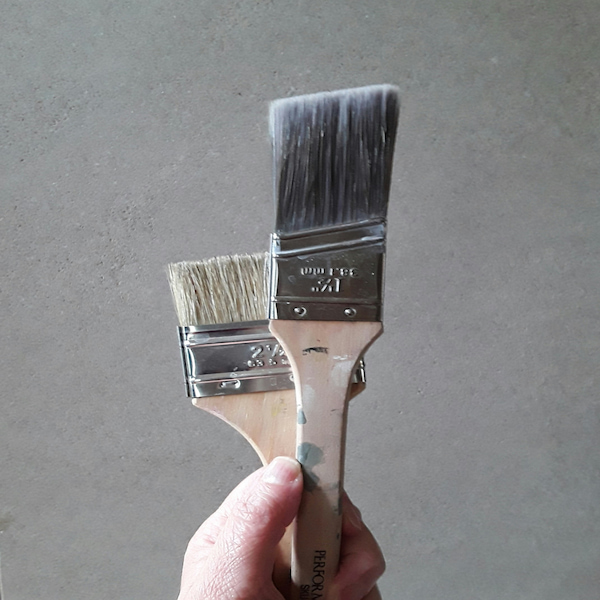
Most manufacturers don’t realize how much raw bristle material they waste on poor dimensional control. A common shortcut is using thicker wedges to reduce bristle volume inside the ferrule. But this practice actually wastes more material than it saves: it causes misaligned bristle insertion, creates tip defects, and forces machines to reject or rework a higher share of units.
From our production experience, keeping the combined wedge and ferrule wall thickness below 0.6 mm is the golden standard. This ratio maximizes bristle retention, minimizes tip defects, and allows automated bristle-setting machines to run at peak efficiency with minimal waste. When your tooling and components are calibrated to this standard, you use exactly the right amount of bristle material—no more, no less.
Labor and downtime are two of the largest costs in any production facility. Low-quality components don’t just hurt product quality—they slow down your entire line. Wooden wedges require frequent machine cleaning to remove splinters, and inconsistent dimensions mean constant setup adjustments.
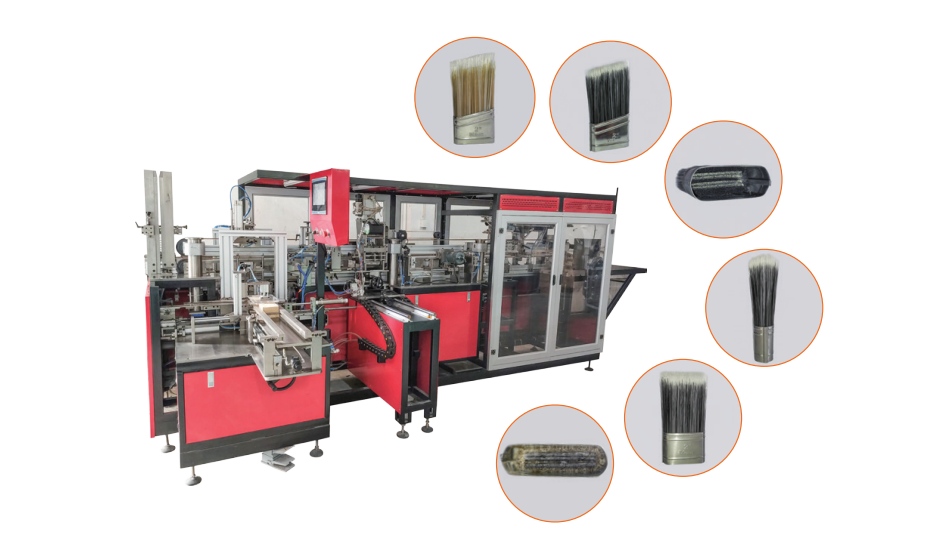
As a manufacturer of both brush-making equipment and PE regrind wedges, we design our components to work seamlessly together. Precision-engineered wedges reduce changeover time, eliminate splinter-related jams, and let your line run faster and longer. Higher throughput with less maintenance means lower cost per unit—without any drop in quality.
Read More



 IPv6 network supported

